Manufacturing & Quality
A module either lasts twenty-five years or it doesn't — and that is decided on the production line, not on the roof.
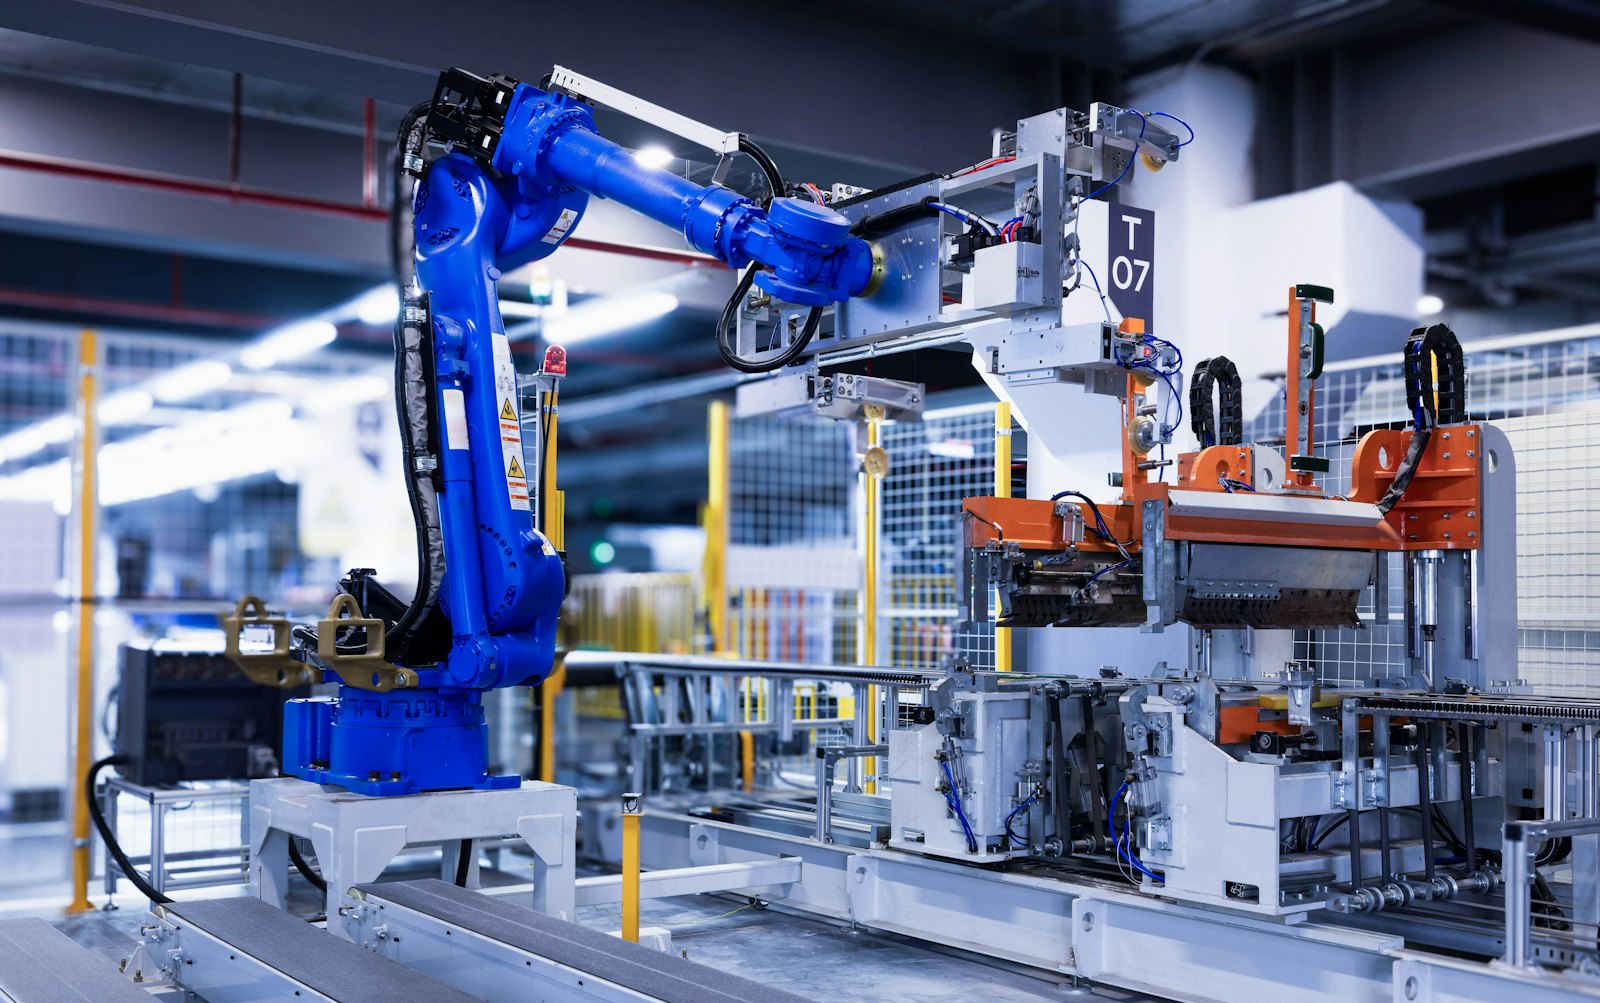
Automate the repeatable. Inspect the critical.
Photovoltaic modules fail in slow, quiet ways: a micro-crack that grows across ten monsoons, a cold solder joint that oxidises, an encapsulant that yellows because the lamination cure ran two degrees low. None of it shows up on day one. All of it shows up on your generation report in year eight.
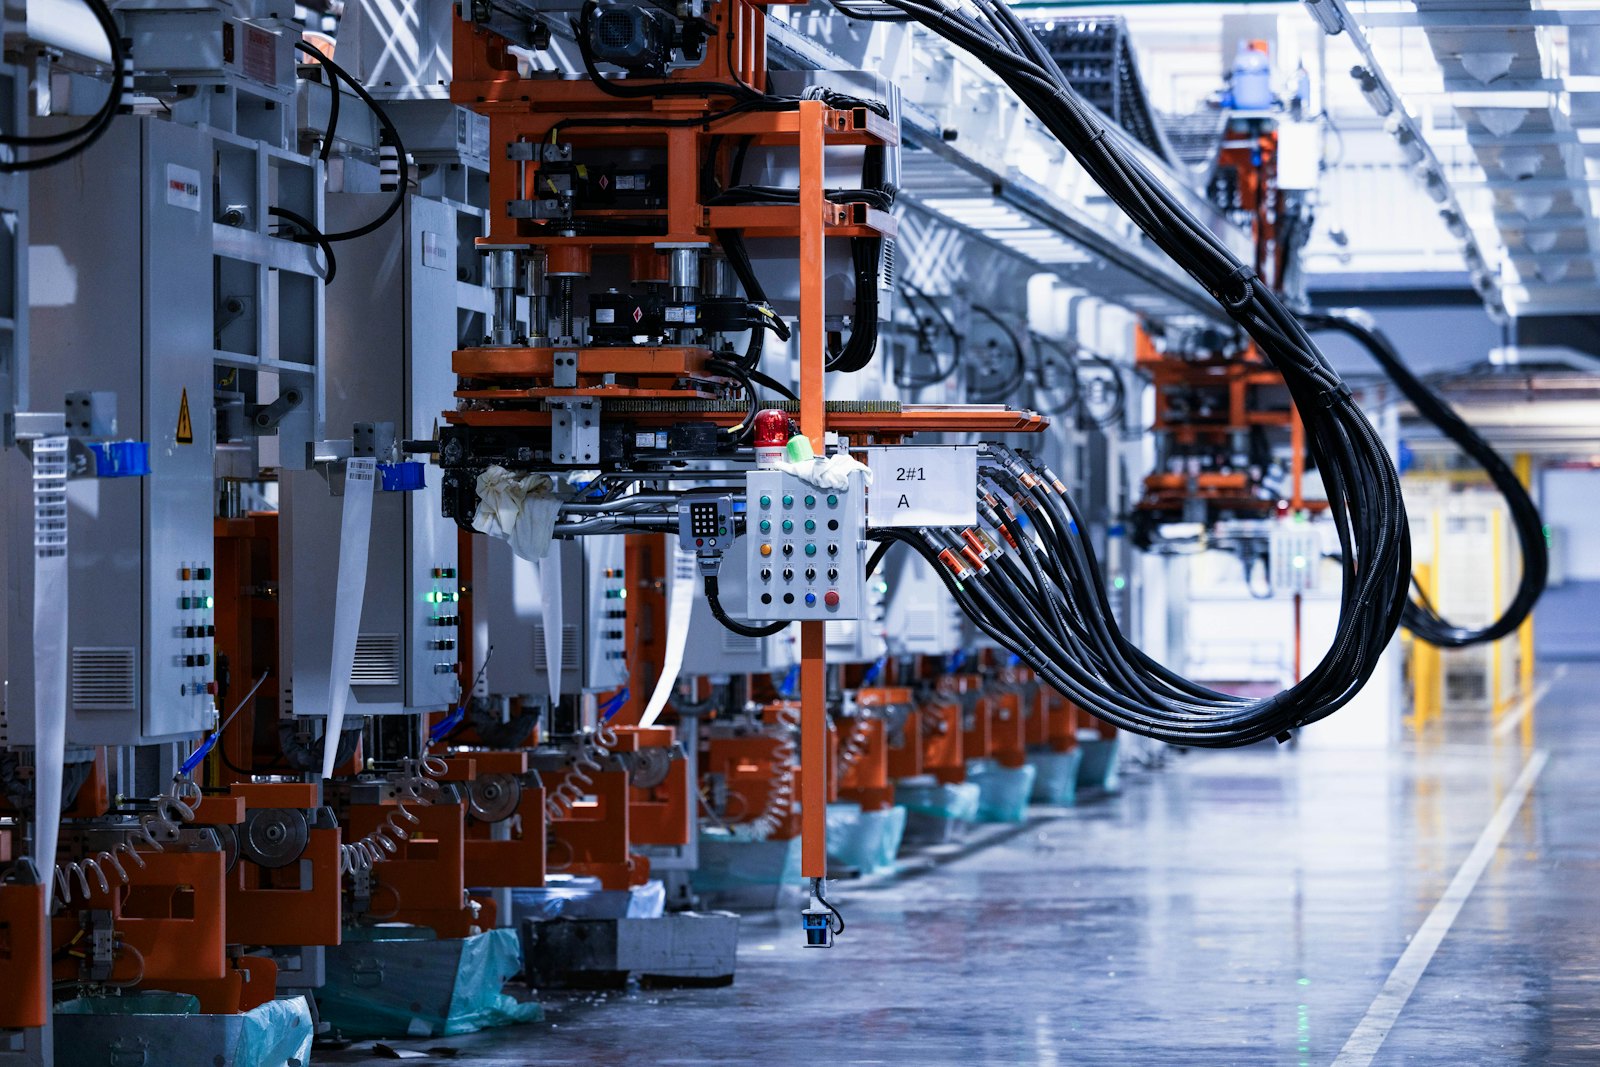
That is why our process concentrates on the handful of variables that actually govern long-term performance — and why every module is imaged and tested individually rather than sampled by batch.
- Automated stringing for consistent solder joint geometry and low cell stress
- Controlled lamination profiles with logged temperature and pressure curves
- Electroluminescence imaging before and after lamination
- Flash testing and power binning at Standard Test Conditions on every unit
- Serial-number traceability from incoming cell batch to dispatched pallet
How a module is made
Eight stages, each with its own hold point. A module that fails a hold point does not move forward.
Cell inspection
Incoming cells are checked for colour uniformity, efficiency class and micro-crack indications before release to the line.
Cell cutting
Laser scribing and cleaving into half-cells, with edge quality checked to limit recombination losses at the cut line.
Stringing
Automated tabbing and stringing under a controlled temperature profile for consistent, low-stress solder joints.
Layup
Glass, encapsulant, cell matrix, encapsulant and backsheet (or rear glass) stacked and bussed to the layout drawing.
Pre-lam EL test
Electroluminescence imaging catches cracks and disconnected fingers before lamination locks the fault in permanently.
Lamination
Vacuum lamination with a logged cure profile, cross-linking the encapsulant into a sealed, moisture-resistant package.
Framing & sealing
Anodised aluminium frame applied with structural sealant; junction box potted and bypass diodes verified.
Final test & binning
Post-lam EL, high-potential insulation test, flash test at STC, power binning, labelling and packing.
What we test, and what you get to see
Quality claims are cheap. Test records are not. With every consignment we hand over the underlying data, so you can hold the product to its specification rather than to our marketing.
- Flash test report — Pmax, Voc, Isc, Vmp, Imp and fill factor for each serial number
- EL images — post-lamination electroluminescence scan of every module
- Insulation & wet leakage — high-potential test results
- Visual inspection record — against a documented defect criteria list
- Packing list — serials mapped to pallet and batch for full traceability
The infrastructure behind the line
Process Control
Lamination, soldering and curing parameters are set, logged and alarmed rather than left to operator judgement.
Automated Inspection
Machine-vision and EL inspection stations flag defects consistently, without the fatigue drift of manual checking.
Traceability
Every serial number resolves back to its cell batch, line, shift and test record for the life of the warranty.
Material Sourcing
Cells, encapsulant, glass, backsheet and junction boxes qualified against specification before approval for use.
Safety Culture
Documented safe working procedures, PPE discipline and electrical isolation protocols on the floor and on site.
Waste & Recycling
Glass cullet, aluminium offcuts and packaging routed to recycling streams rather than to landfill.
From line to loading bay
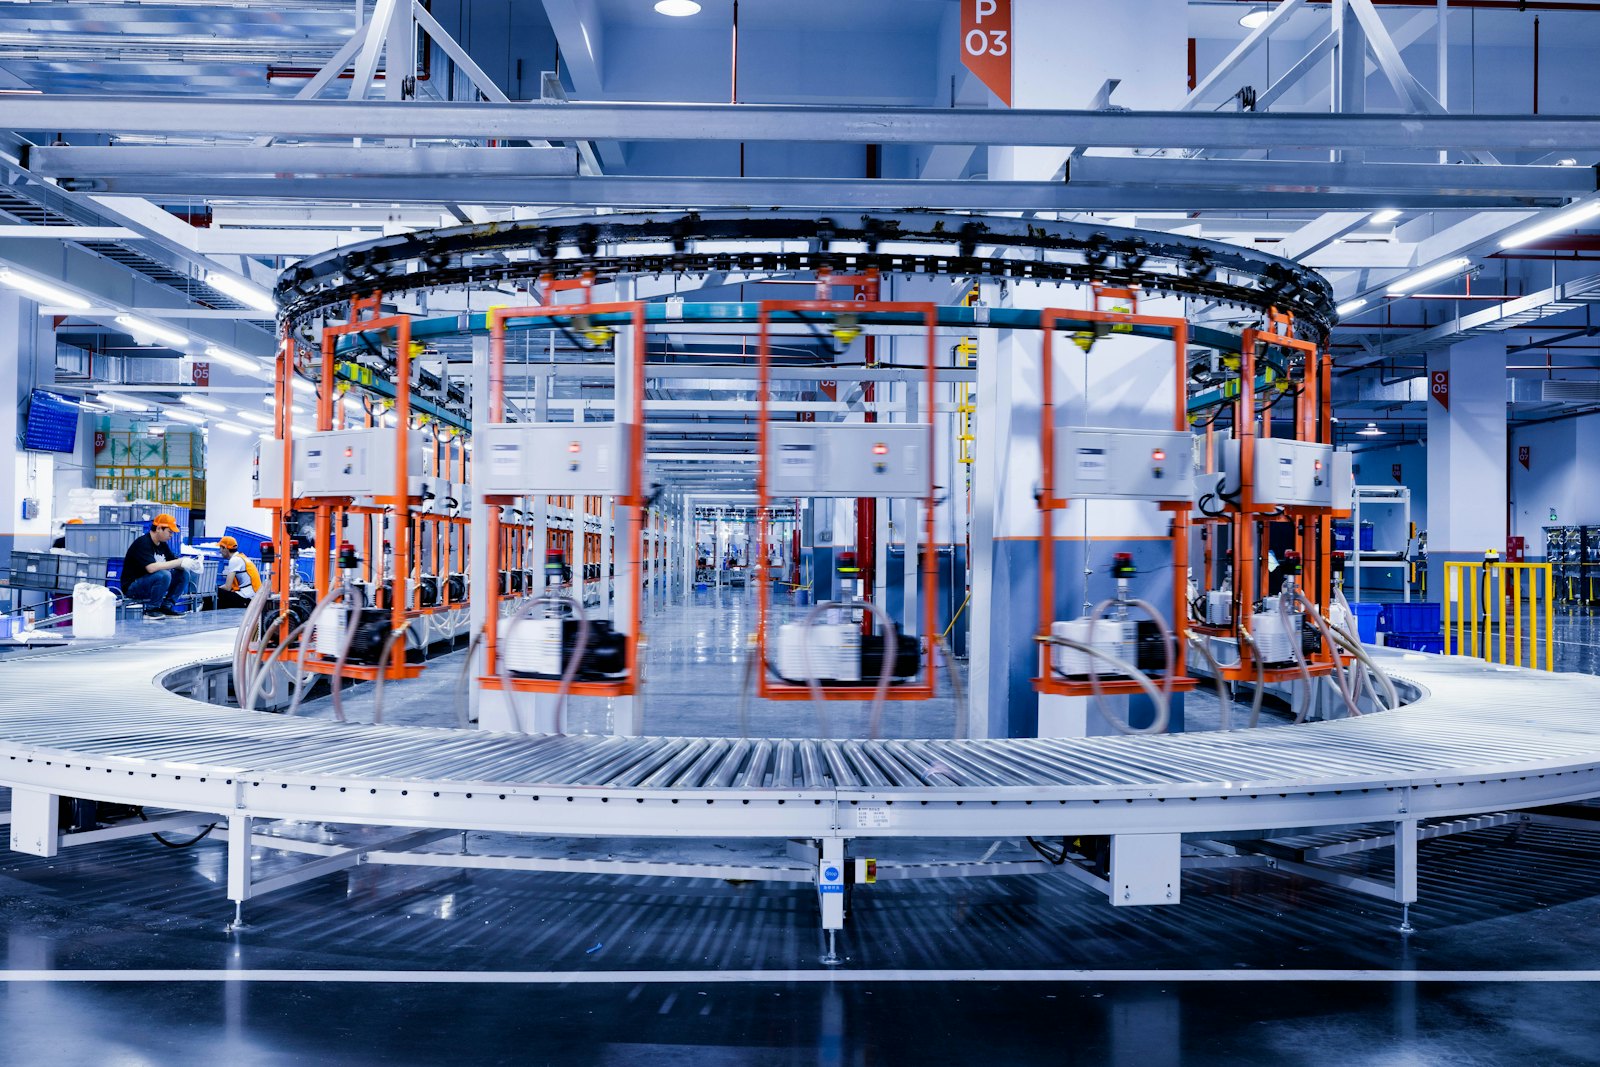
Assembly, inspection and dispatch — the three stages every module passes through before it reaches your site.
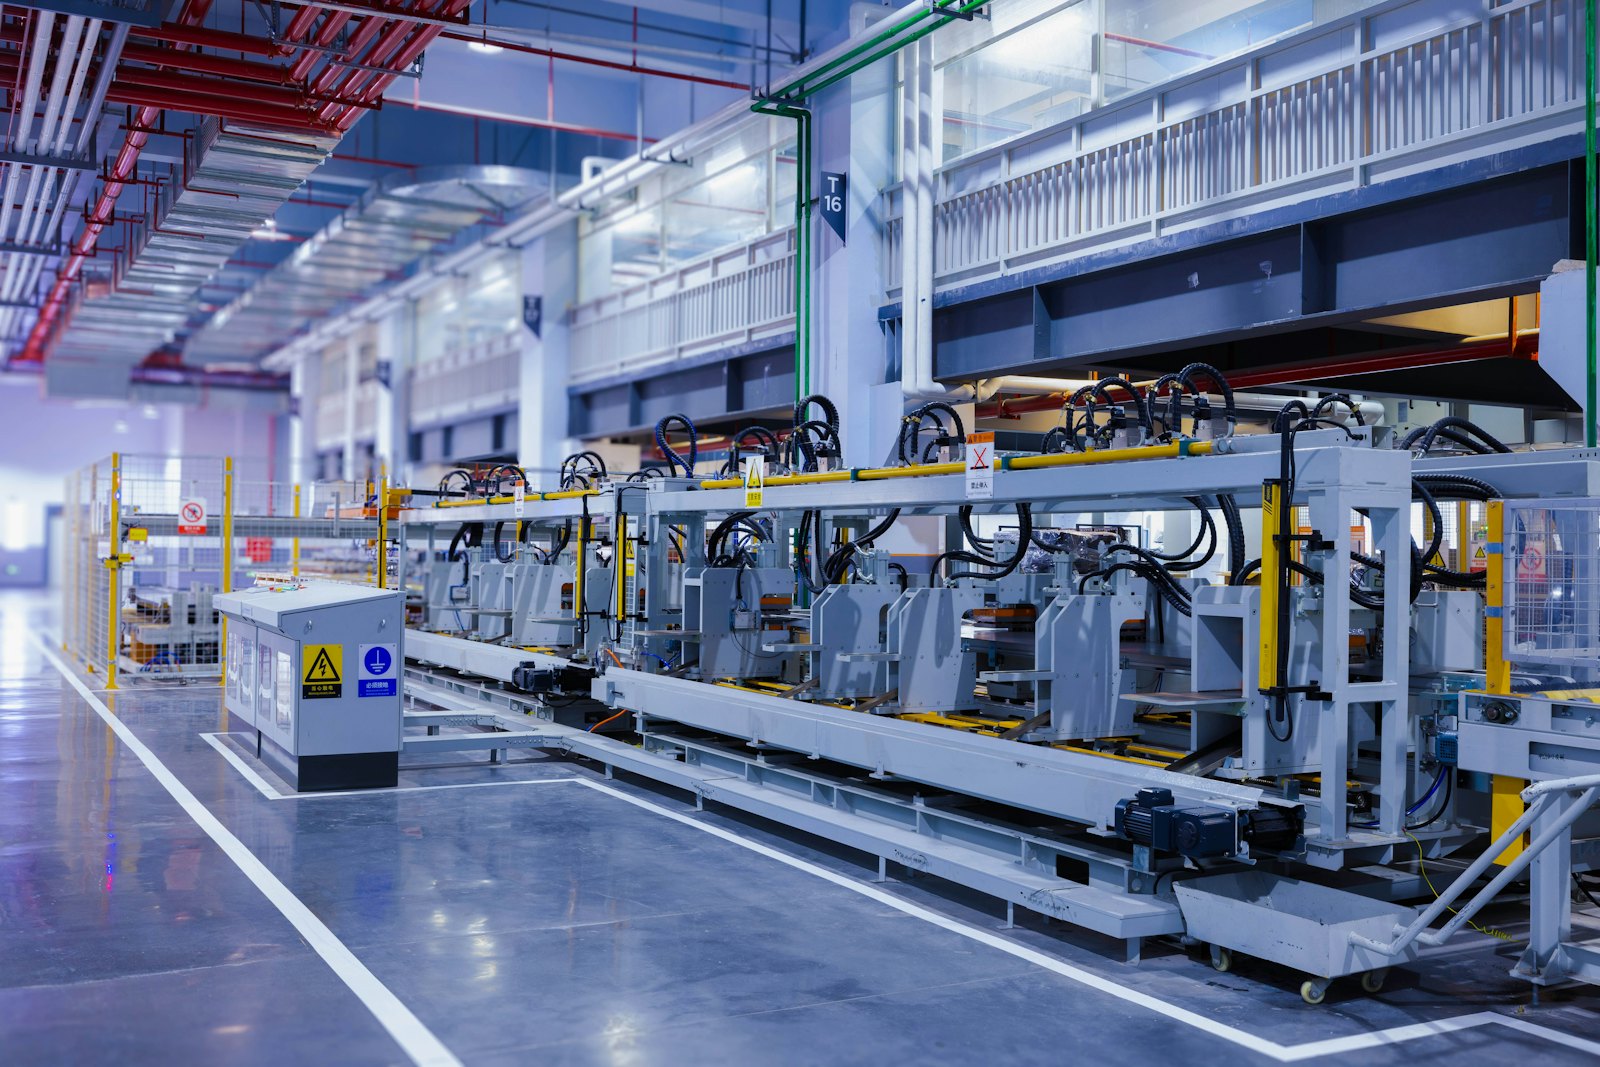
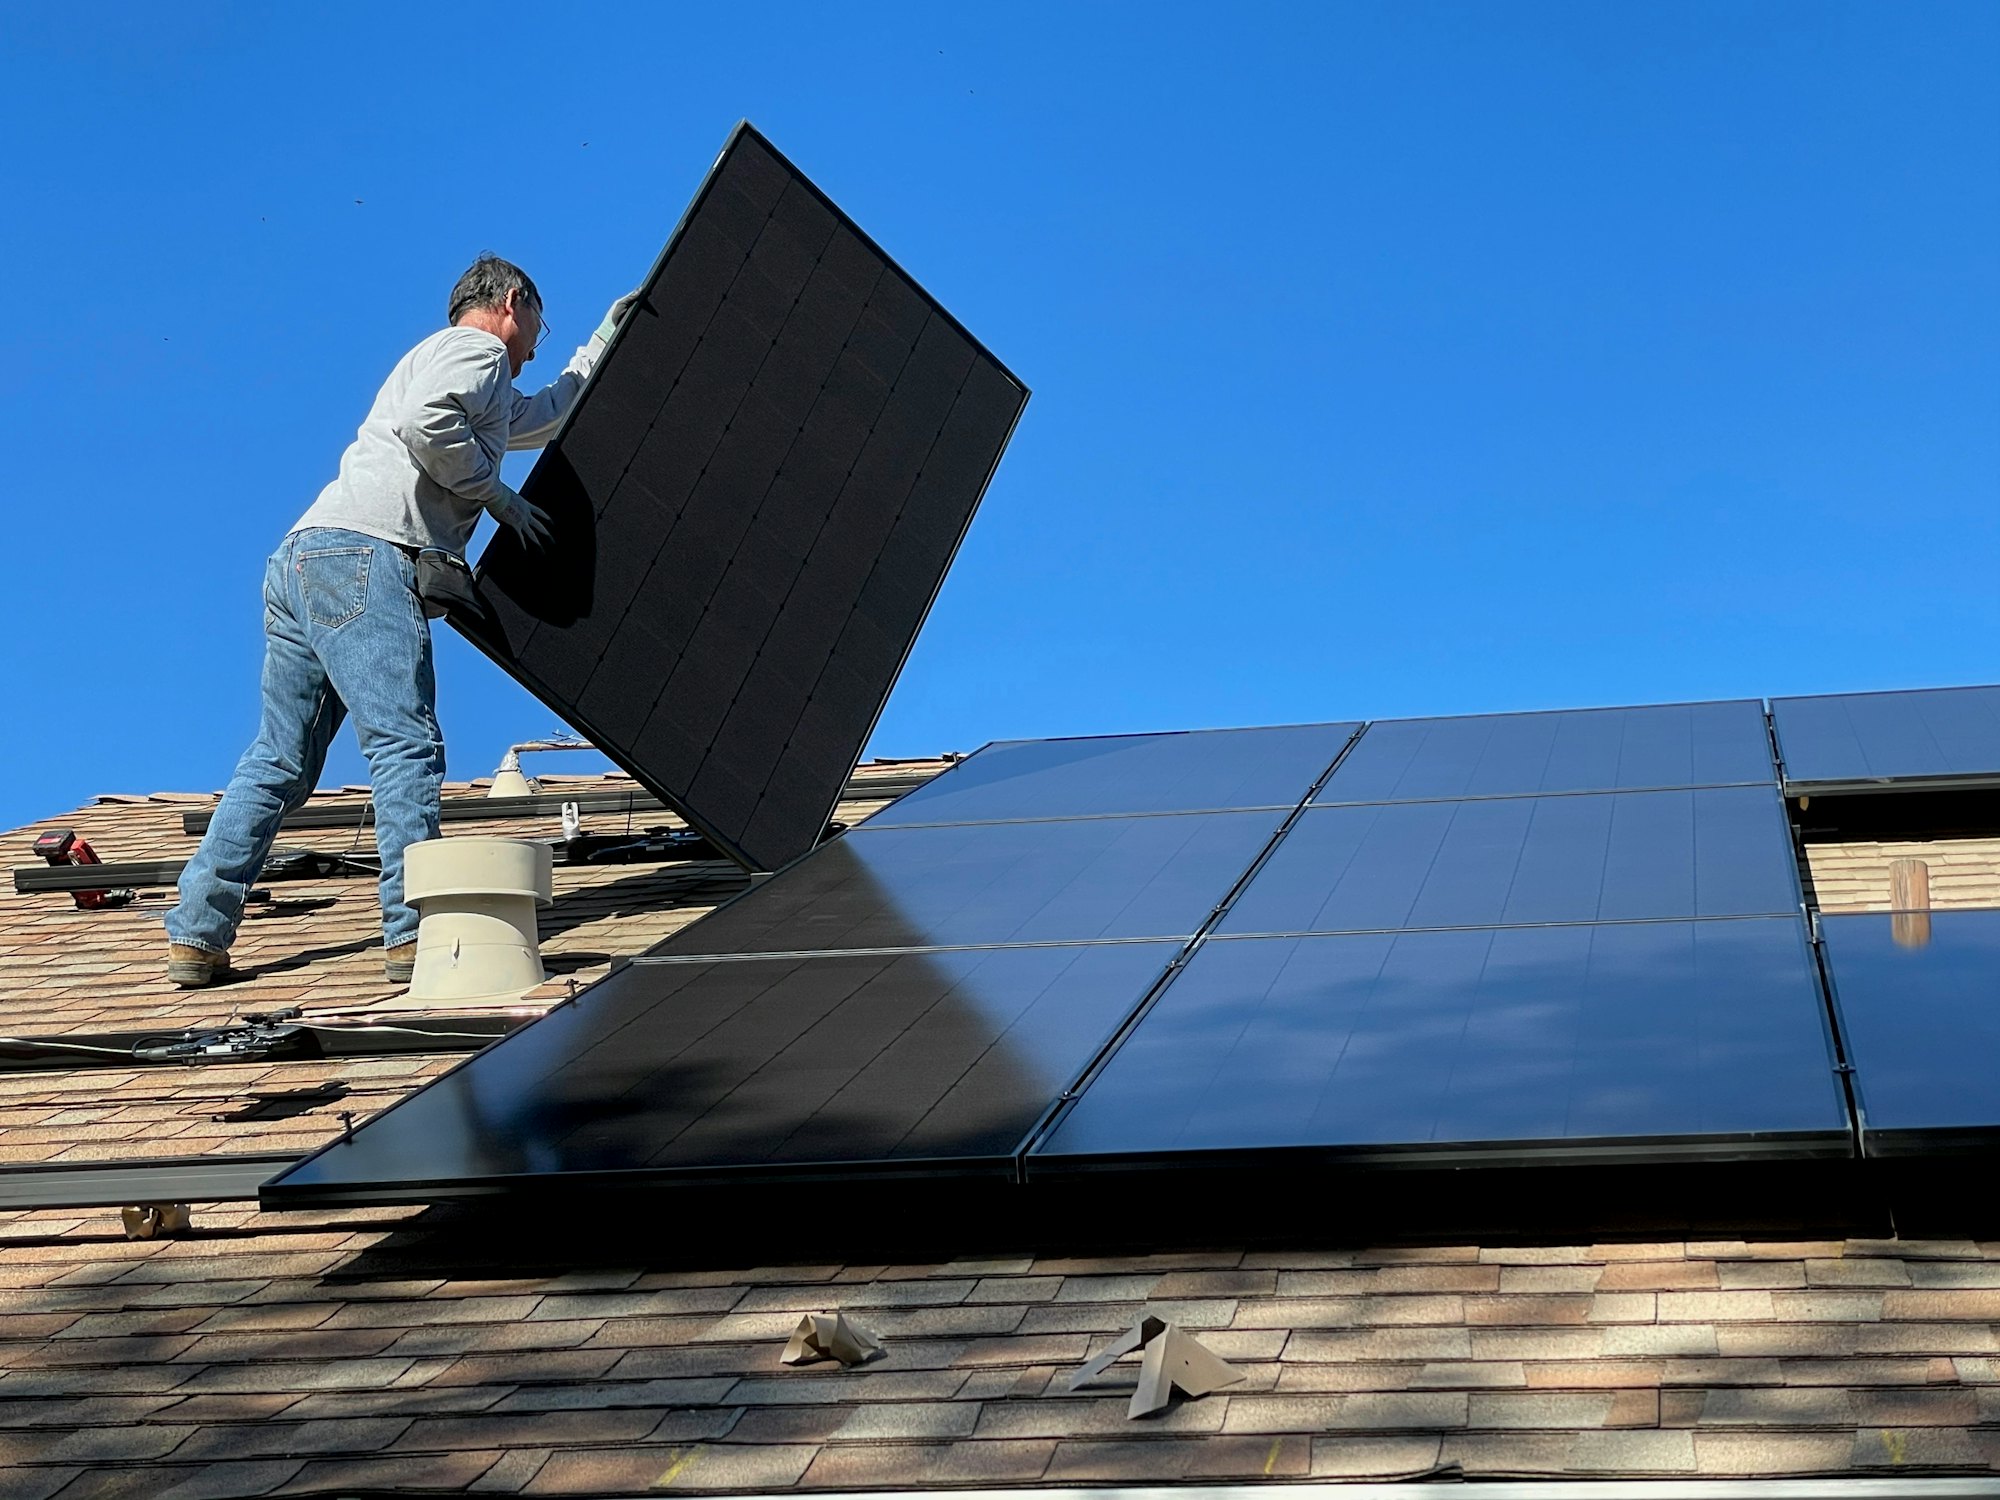
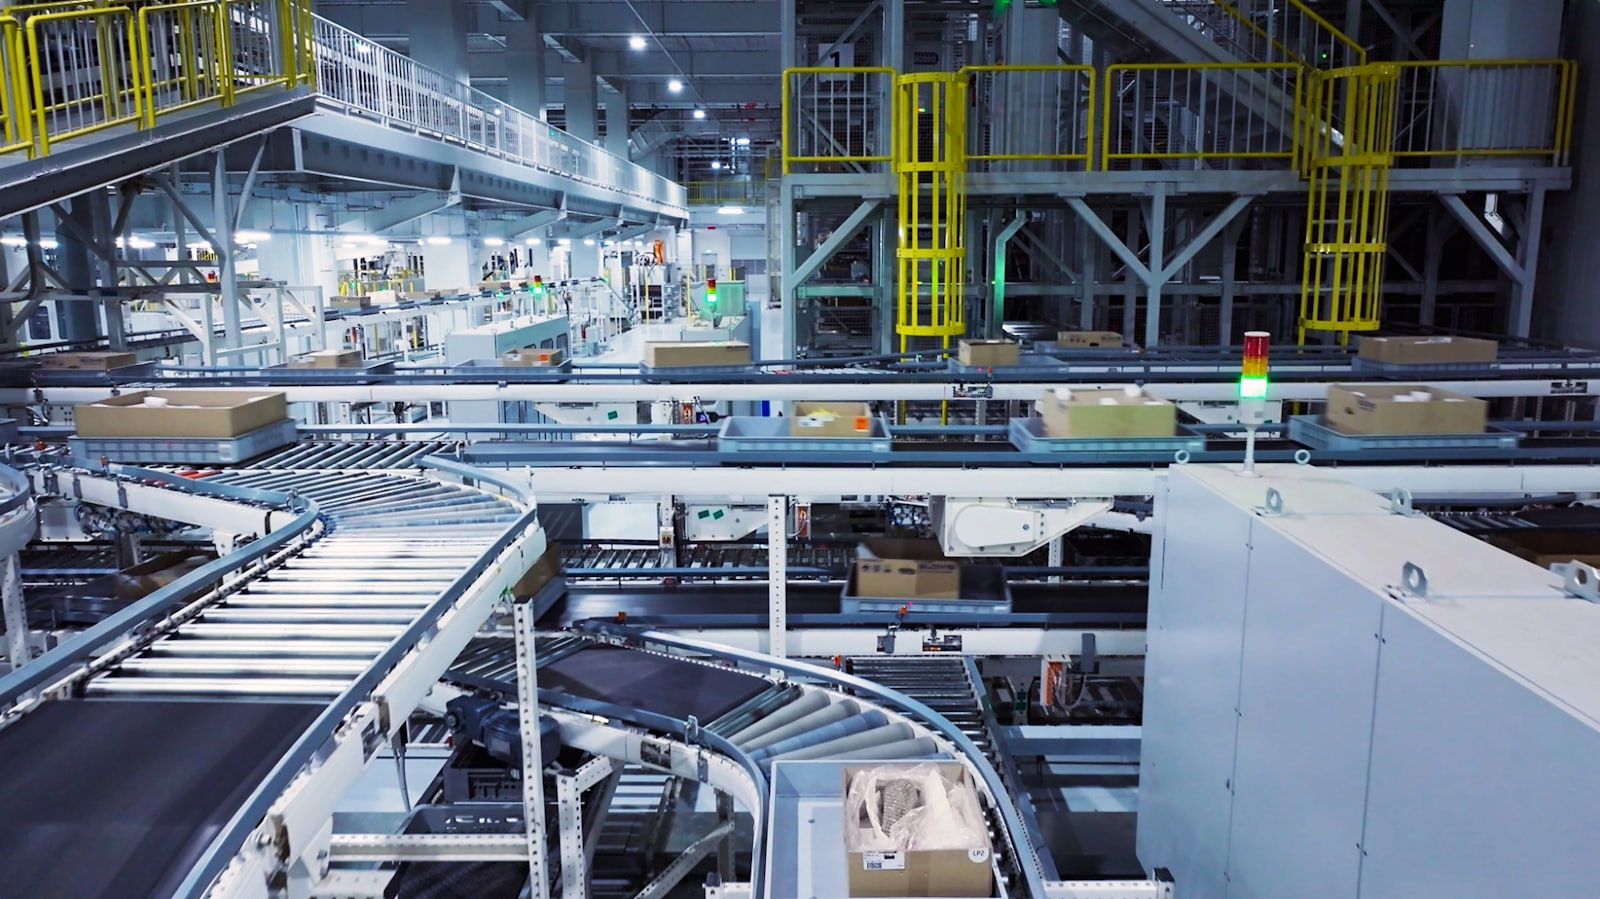
Representative images. Photographs of our own facility will replace these once the plant is operational.
Site owner note: this page describes the manufacturing process and quality regime in general terms and does not state a production capacity, plant address or commissioning date. Add those specifics — along with genuine photographs of your own facility to replace the stock images — once the plant is operational. Do not publish a capacity figure until it is real; it is the first thing a serious buyer will ask you to demonstrate.